
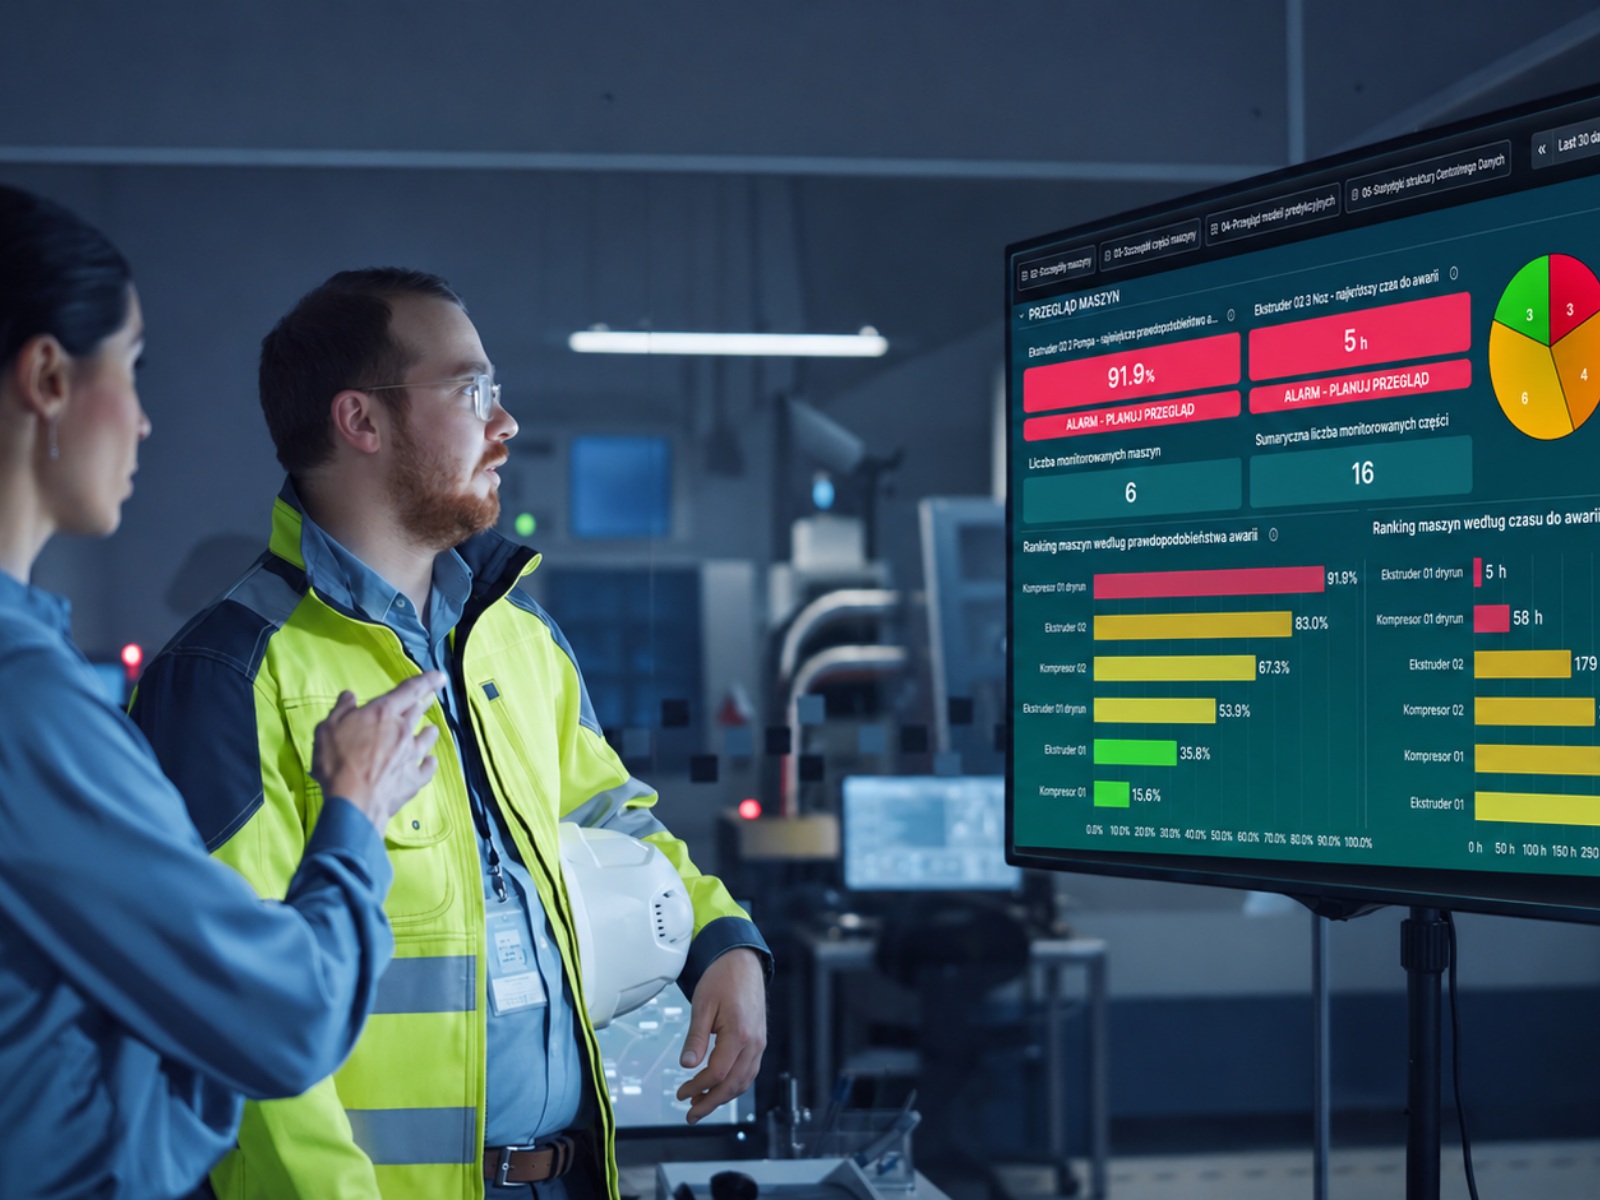
Industrial maintenance in a manufacturing plant: role, strategies, KPIs and tools

Gabriela Gic-Grusza
Industrial maintenance is the set of technical, organisational and managerial activities that keep machines, equipment and infrastructure capable of performing their required functions – or restore that capability after a failure. In a manufacturing plant, maintenance owns production continuity, downtime reduction, safety, cost control and the reliability of the asset base.
In practice, maintenance is far more than fixing things after they break. A modern maintenance function plans inspections, analyses failures, manages spare parts, monitors equipment condition, supports operators, works in a CMMS, and increasingly relies on sensor data, analytics and Industry 4.0 tooling.
What is industrial maintenance?
Industrial maintenance is the discipline responsible for the technical condition of machines, equipment, installations and plant infrastructure.
The objective is straightforward: production should run safely, steadily and predictably. That means fewer unplanned stoppages, longer asset life, controlled repair costs, well-planned spare parts and fast recovery when a failure does occur.
Industrial maintenance typically covers:
- servicing of machines and equipment;
- breakdown repairs;
- periodic inspections;
- planning of preventive activities;
- technical diagnostics;
- equipment condition monitoring;
- failure root-cause analysis;
- technical upgrades and retrofits;
- spare parts management;
- technical documentation;
- cooperation with production, quality, procurement and IT;
- maintenance KPI reporting.
In a well-run plant, maintenance does not operate alongside production – it operates with it. Maintenance decisions shape line availability, product quality, workplace safety, energy consumption and unit production cost.
The maintenance department – structure, roles and responsibilities
The maintenance department is the organisational unit accountable for the technical condition of the machine park and the production infrastructure.
Depending on plant size, it may consist of a handful of people or a full structure covering mechanics, electricians, control engineers, planners, reliability engineers, a spare parts store, diagnostics specialists and a maintenance manager.
| Role | Core responsibilities | Key competencies |
| Maintenance technician | Day-to-day servicing, repairs, inspections, breakdown response | Mechanics, electrics, pneumatics, hydraulics, basic diagnostics |
| Control and automation technician | Diagnostics of control systems, PLCs, sensors, drives and automation | PLC, HMI, inverters, industrial networks, signal analysis |
| Maintenance engineer | Inspection planning, failure analysis, optimisation of maintenance strategy | Data analysis, reliability, FMEA, RCA, CMMS, KPIs |
| Maintenance planner | Work schedules, resource planning, parts and service windows | Planning, CMMS, coordination, prioritisation |
| Maintenance manager | Strategy, budget, KPIs, team, priorities, cross-functional cooperation | Management, engineering, finance, communication, risk analysis |
| Spare parts store | Parts availability, minimum stock levels, ordering, inventory turnover | Inventory management, ERP, part identification, cost control |
Maintenance works most closely with production, quality, procurement and IT. Production reports problems and releases service windows. Quality flags deviations linked to equipment condition. Procurement secures parts and external services. IT and automation support the CMMS, data integration, IoT and cybersecurity.
Maintenance competencies increasingly reach beyond classic mechanics and electrics. Alongside hands-on technical skills, teams need working knowledge of automation, PLCs, sensors, data analysis, digital systems and reliability fundamentals.
Responsibilities of the maintenance department
Maintenance responsibilities span both day-to-day technical work and the planning, analysis and continuous improvement of how the asset base is managed.
The core responsibilities are:
| Area | Responsibilities |
| Day-to-day maintenance | Breakdown response, fault clearing, restoring equipment to service |
| Servicing | Lubrication, cleaning, adjustments, inspection of wear parts |
| Inspections | Planning and execution of periodic inspections |
| Diagnostics | Measurements, symptom analysis, testing, fault localisation |
| Planning | Work schedules, service windows, resources, parts |
| Parts management | Stock levels, critical parts, alternatives, purchase orders |
| Documentation | Repair history, reports, work instructions, asset records |
| Failure analysis | Root-cause identification, repeat failures, corrective actions |
| Upgrades | Technical improvements, elimination of weak points, safety enhancements |
| Cooperation with production | Task prioritisation, downtime planning, operator support |
| Reporting | MTBF, MTTR, OEE, costs, failure rate, share of planned work |
A mature maintenance function does more than repair machines. It analyses why failures occur, which assets are critical, where inspections are too frequent, where response is too slow, and which actions genuinely improve reliability.
Maintenance strategies
A maintenance strategy defines when and why the maintenance team acts. The right choice depends on asset criticality, the cost of failure, parts availability, safety requirements, data availability and organisational maturity.
Five approaches are commonly distinguished:
- reactive maintenance;
- preventive maintenance;
- predictive maintenance;
- proactive maintenance;
- autonomous maintenance.
Reactive maintenance
Reactive maintenance means repairing equipment after it fails. It is the simplest approach to organise and carries the lowest up-front cost, but on critical assets it can drive high downtime costs, emergency labour and secondary damage.
It makes sense mainly for inexpensive components that are easy to replace and non-critical to production.
Preventive maintenance
Preventive maintenance delivers inspections, servicing and replacements on a fixed schedule – calendar time, running hours or cycles.
It reduces failure risk compared with a reactive approach, but it can lead to over-maintenance when parts are replaced while still in good condition.
Predictive maintenance
Predictive maintenance (PdM) uses sensor data, industrial systems and analytical models to estimate failure risk or the time available before intervention is required.
It depends on data, condition monitoring, analytics and a defined response process. The business case is strongest for critical, high-value assets whose degradation can be detected through technical signals.
Proactive maintenance
Proactive maintenance focuses on eliminating the root causes of failure rather than repairing their consequences.
In practice it draws on root-cause analysis, FMEA, RCM, repeat-failure reviews, design modifications, improved procedures and changes to how equipment is operated. The goal is a durable improvement in reliability, not simply a faster response.
Autonomous maintenance
Autonomous maintenance brings operators into the basic care of their equipment: cleaning, inspection, reporting abnormalities, simple adjustments and maintaining workplace standards.
It is one of the pillars of Total Productive Maintenance (TPM). It does not replace the maintenance department, but it surfaces deviations earlier and builds shared ownership of equipment condition.
Comparing maintenance strategies
There is no single best strategy for every machine. What is right for a low-cost auxiliary component is wrong for a critical compressor, robot, furnace, pump, packaging line or safety system.
| Dimension | Reactive | Preventive | Predictive | Proactive | Autonomous |
| Trigger | Failure | Schedule | Sensor data and analytics | Root-cause analysis | Operator routine |
| Cost profile | Low up-front cost, often high total cost | Moderate | Higher up-front cost, potentially lower failure cost | Moderate to high | Low direct cost, requires investment in training and standards |
| Data requirements | Minimal | Calendar, running hours, OEM recommendations | Sensors, failure history, process data, models | Failure data, RCA, FMEA, RCM | Checklists, observations, standards |
| Effect on downtime | High risk of unplanned stoppages | Part of downtime becomes planned | More targeted action ahead of failure | Long-term reduction in failures | Early detection of abnormalities |
| Best suited to | Non-critical assets | Known wear patterns, mandatory inspections | Critical assets whose condition can be monitored | Repeat failures, high organisational maturity | Areas where operators work with the machine daily |
| Maturity level | Basic | Developing | Advanced | Optimising | Element of TPM culture |
Strategy selection should start with asset criticality. Machines whose failure stops production or creates a safety risk warrant a different approach from auxiliary equipment whose failure does not affect the process.
The maintenance maturity path
Maintenance typically evolves from reactive firefighting towards management based on data, causes and risk.
The maturity path can be summarised as follows:
reactive maintenance → preventive maintenance → predictive maintenance → proactive maintenance → smart maintenance
Autonomous maintenance is not a separate stage on this path. It is an element of TPM culture that can accompany any level of maturity.
At the reactive level, the organisation mostly clears breakdowns. At the preventive level, it plans work and builds schedules. At the predictive level, it uses equipment condition data. At the proactive level, it removes root causes and optimises strategies for whole asset classes.
| Level | Characteristics | Typical tooling |
| 1 | Response after failure | Fault reports, simple work orders, technician know-how |
| 2 | Planned inspections | Schedules, CMMS, basic KPIs |
| 3 | Monitoring and prediction | Sensors, IoT, condition monitoring, analytics |
| 4 | Reliability optimisation | RCM, FMEA, RCA, cost analysis, per-asset strategies |
| 5 | Smart maintenance | Data, decision automation, maintenance integrated with production and the business |
Not every organisation needs to reach the top level immediately. What matters is that the strategy matches the risk, cost and importance of the assets involved.
Maintenance KPIs
Maintenance KPIs measure the effectiveness of the maintenance function, equipment reliability, response speed, cost and impact on production.
| KPI | What it shows | Reference value / interpretation |
| Overall Equipment Effectiveness (OEE) | Utilisation of equipment; maintenance mainly influences availability | A world-class benchmark of >85% is often quoted, but the result depends on industry and process |
| Mean Time Between Failures (MTBF) | Asset reliability | MTBF has no universal target – it is assessed against the history of a given asset type and its trend over time, not against other equipment or industries |
| Mean Time To Repair (MTTR) | Speed of restoring equipment to service | The lower the trend, the better the response and the organisation’s readiness |
| Failure rate | Number of failures per unit of time or output | The aim is a downward trend, particularly on critical assets |
| Maintenance cost | Maintenance spend relative to the replacement asset value | A widely used benchmark is 2–5% of replacement asset value per year |
| Share of planned work | Ratio of planned to unplanned work | Many organisations target >80% planned work |
| Asset availability | Share of time an asset is available for production | A key measure of the maintenance contribution to production continuity |
| Cost of downtime | Production or financial loss caused by a stoppage | Helps establish asset criticality and maintenance priorities |
| PM compliance | Share of preventive work completed as planned | High compliance indicates discipline in planning and execution |
| Repeat failures | Recurring problems on the same assets | Signals the need for RCA, FMEA, RCM or a technical upgrade |
KPIs should never be read in isolation. A low MTTR can look impressive, but if MTBF is falling the organisation is simply repairing failures that occur too often. High PM compliance is not enough if the inspection schedule does not reduce the number of failures.
Systems and tools in maintenance
A maintenance system should support the planning, execution and analysis of maintenance work. The usual foundation is a CMMS – a Computerized Maintenance Management System.
A CMMS typically supports:
- fault reporting;
- work order handling;
- inspection schedules;
- planning of preventive work;
- failure history;
- resource assignment;
- spare parts management;
- asset documentation;
- KPI reporting;
- maintenance cost analysis;
- integration with ERP, MES or a data platform.
Beyond the CMMS, IoT sensors, SCADA systems, historians, MES, industrial data platforms and analytics tooling play a growing role. Data integration makes it possible to combine information on equipment condition, production, quality, energy, alarms and maintenance work orders.
A typical data flow in a modern maintenance setup:
sensor / machine → SCADA / historian → data platform → analytics → alert → CMMS → work order → verification of the outcome
In this model the CMMS runs the execution process, while the data platform and analytics layer detect deviations, trends and emerging failure risk.
Maintenance and Industry 4.0
Industry 4.0 is shifting maintenance from a largely reactive activity towards a process driven by data, condition monitoring and risk analysis.
The technologies that matter most here are:
- the Internet of Things (IoT);
- vibration, temperature, pressure and current sensors;
- condition monitoring;
- artificial intelligence (AI);
- machine learning (ML);
- anomaly detection;
- Remaining Useful Life (RUL) estimation;
- edge computing;
- cloud computing;
- digital twins;
- industrial data platforms.
Smart maintenance is about connecting data, analytics and operational action. Collecting signals from machines is not the point. The point is that data should lead to a decision: an inspection, a schedule change, a parts order, a load reduction, a work order or a root-cause investigation.
The maintenance role itself is changing too. Technicians still need mechanical, electrical and automation skills, but increasingly they also need to read data, alarms and trend charts, and to understand how the digital systems around the asset work.
Smart RDM in the context of smart maintenance
Smart RDM supports smart maintenance as a platform that brings industrial data, analytics and operational action together.
In practice, that means combining data from sensors, SCADA systems, historians, production, quality, energy and maintenance systems within a single asset and process context.
Smart RDM can support areas such as:
- equipment condition monitoring;
- trend and deviation analysis;
- operational alarms and events;
- integration of data from multiple sources;
- KPI dashboards;
- analysis of failure impact on production;
- input data for predictive maintenance;
- decision support for inspections, interventions and corrective actions.
Smart RDM does not replace the maintenance department, nor is it a CMMS. It acts as the data and analytics layer that helps maintenance, production and management teams decide on the basis of shared, current information.
Related topics in the maintenance cluster
Maintenance is a broad field, and many of its topics deserve their own, more detailed guides. This article works as the entry point to the wider maintenance content cluster.
| Topic | What it covers |
| Predictive maintenance | Models, data and processes for predicting failures |
| Condition-based maintenance | Maintenance decisions triggered by the technical condition of an asset |
| Condition monitoring | Measurement techniques such as vibration, temperature, oil analysis and ultrasound |
| RCM | Matching maintenance strategy to asset function, failure mode and consequences |
| FMEA | Analysis of failure modes and their effects |
| MTBF and MTTR | Reliability and response-speed indicators |
| Maintenance KPIs | Measures of maintenance effectiveness, cost, planning and reliability |
| Autonomous maintenance | The operator’s role in day-to-day equipment care |
| Plant maintenance software | CMMS systems and tooling for managing maintenance work |
| Asset Performance Management | Managing asset performance, health and risk |
| Alarm management | Managing alarms, priorities and operator response |
| Types of maintenance | The full taxonomy of maintenance strategies |
| Preventive vs predictive | Comparison of schedule-based and data-driven approaches |
| Predictive analytics platform | Data and models that support failure prediction |
| OEE | How equipment availability affects production performance |
| Industrial data platform | Integration of data from machines, systems and processes |
Splitting the subject this way avoids the trap of one article trying to explain all of maintenance at too high a level. Maintenance needs both an organisational perspective and dedicated guides to strategies, KPIs, data, systems and analysis methods.
Standards relevant to maintenance
A handful of standards are worth knowing, as they bring order to maintenance terminology, KPIs and asset management.
| Standard | Scope |
| EN 13306 | Maintenance terminology |
| EN 15341 | Maintenance key performance indicators |
| ISO 55000 | Asset management: principles, terminology and system approach |
| ISO 55001 | Requirements for an asset management system |
| ISO 55002 | Guidelines for the application of ISO 55001 |
Standards do not replace the practical knowledge of a maintenance team, but they do align language, metrics and the way assets are managed. They are especially useful in multi-site organisations, in audited environments, and wherever results need to be compared across sites.
How to improve maintenance in a manufacturing plant
Improvement should start with putting assets, fault reports, work orders, KPIs and failure data in order.
A practical sequence looks like this:
| Step | Action | Outcome |
| 1 | Build an asset register and equipment hierarchy | You know what you maintain and which assets are critical |
| 2 | Standardise fault reports and work orders | Repair history becomes analysable |
| 3 | Introduce a basic KPI set | MTBF, MTTR, cost, failure rate and availability become measurable |
| 4 | Define asset criticality | Maintenance strategy is matched to risk |
| 5 | Separate reactive, preventive and predictive work | The structure of the team’s workload becomes visible |
| 6 | Organise the spare parts store | Faster response and lower risk of missing parts |
| 7 | Involve operators in basic checks | Problems are detected earlier |
| 8 | Collect data from machines and systems | The foundation for condition monitoring and prediction |
| 9 | Analyse repeat failures | Root causes can be removed permanently |
| 10 | Review the strategy on a regular cycle | The maintenance programme stays aligned with process changes |
The greatest value comes from combining solid basics with data. If work orders are poorly described, parts have no item numbers and failures are not classified, predictive maintenance will not work. Data and process discipline come first.
FAQ
What does industrial maintenance mean in practice?
It is the set of technical, organisational and managerial activities that keep machines, equipment and plant infrastructure serviceable. The aim is production continuity, less downtime, safety, cost control and the preservation of required asset functions.
Day to day, that covers repairs, inspections, servicing, diagnostics, monitoring, planning, spare parts, documentation and failure analysis.
What is the maintenance department responsible for?
Servicing, repairs, inspections, work planning, parts management, diagnostics, documentation, failure analysis, technical upgrades and KPI reporting.
It works with production, quality, procurement and IT, because equipment condition drives production continuity, quality, cost, safety and operational data.
What does a maintenance technician do?
A maintenance technician diagnoses faults, clears breakdowns, carries out inspections and servicing, checks the technical condition of equipment and documents the work performed.
Depending on the role, the focus may be mechanics, electrics, automation, PLCs, diagnostics, data analysis, inspection planning or parts management.
Which maintenance strategies are there?
The five commonly distinguished approaches are reactive, preventive, predictive, proactive and autonomous maintenance.
Reactive acts after failure. Preventive follows a schedule. Predictive uses data and analytics. Proactive removes root causes. Autonomous involves operators in basic inspection and care.
How does preventive maintenance differ from predictive maintenance?
Preventive maintenance follows a schedule – every set number of days, running hours or cycles. Predictive maintenance acts on sensor data, trends and analytical models.
Put simply: prevention asks “is it due?”, while prediction asks “does the data show rising failure risk?”.
How do you measure maintenance performance?
Through OEE, MTBF, MTTR, failure rate, share of planned work, maintenance cost, asset availability, cost of downtime and the number of repeat failures.
What matters most is reading trends and the relationships between indicators. No single KPI captures the effectiveness of a maintenance function.
Which maintenance management system should you choose?
The usual foundation is a CMMS covering work orders, inspections, repair history, the spare parts store, schedules and KPI reporting.
A good system offers a clear asset register, quick work-order creation, integration with ERP or MES, solid reporting, spare parts handling and the ability to work with data from machines and industrial systems.
How is Industry 4.0 changing maintenance?
Industry 4.0 moves maintenance from post-failure response towards decisions based on data, condition monitoring and prediction.
IoT, AI, ML, edge computing, digital twins and data platforms make it possible to detect deviations earlier, analyse trends, assess failure risk and plan work more effectively.
Where should a plant start when improving maintenance?
Start with the basics: asset register, work orders, failure history, spare parts, KPIs and asset criticality.
Condition monitoring, prediction, analytics and automation come next. Without good data quality, even advanced tooling will not improve maintenance performance.
What is autonomous maintenance?
An approach in which operators perform basic equipment care: cleaning, inspection, simple adjustments, reporting deviations and maintaining workplace standards.
It is an element of TPM and does not replace the maintenance department. What it does is surface problems faster and build shared ownership of equipment condition.
How much does maintenance cost?
Maintenance cost depends on the industry, the age of the machine park, asset criticality, the level of automation, parts cost, failure volume, work organisation and the share of planned activity.
A frequently used reference point is 2–5% of replacement asset value per year, though the figure should always be interpreted in the context of the specific plant.
What can you earn in maintenance?
Pay depends on the role, experience, location, industry, shift pattern and technical specialisation. A maintenance technician, a control engineer, a reliability engineer, a planner and a maintenance manager all sit in different bands.
The highest premiums usually go to skills in automation, PLCs, diagnostics, robotics, data analysis and team leadership. Current ranges are best verified against live job postings and salary reports.
Sources
- EN 13306 – maintenance terminology.
- EN 15341 – maintenance key performance indicators.
- ISO 55000 – asset management: principles and terminology.
- ISO 55001 – requirements for an asset management system.
- ISO 55002 – guidelines for the application of ISO 55001.
- Industry publications on CMMS, maintenance KPIs, MTBF, MTTR, OEE, TPM, RCM, FMEA and maintenance strategy.
- Industry publications on Industry 4.0, IoT, AI, ML, condition monitoring and predictive maintenance.
- Smart RDM internal materials on industrial data, asset monitoring, operational analytics, KPIs and smart maintenance.
Light mode