
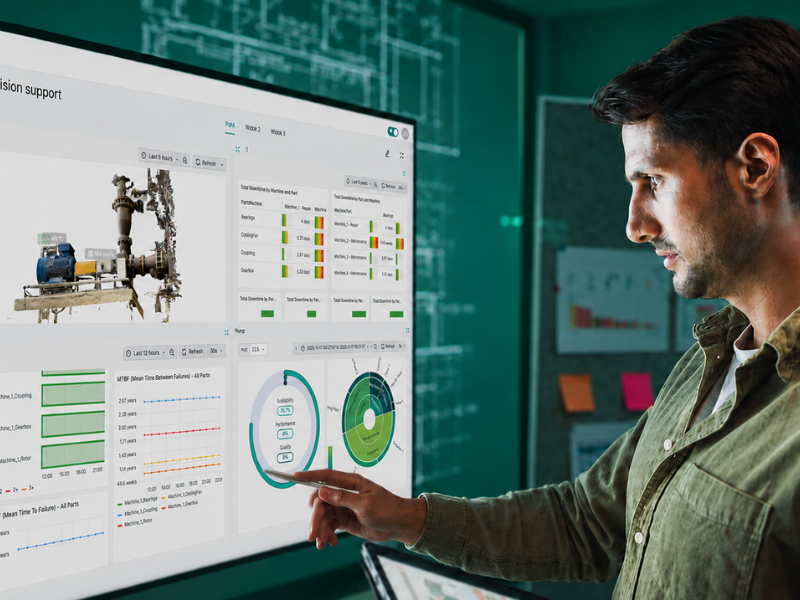
What is Predictive Maintenance? Complete guide
Sebastian Dudzik
Predictive maintenance is a data-driven maintenance strategy that uses equipment condition data, sensor readings, and analytical models to predict when an asset is likely to fail or require service. Instead of maintaining equipment only after it breaks down, or on fixed calendar intervals, predictive maintenance helps teams act before functional failure occurs.
In practical terms, predictive maintenance answers one question:
What maintenance should be done, on which asset, and when, based on evidence from the equipment itself?
This makes predictive maintenance different from traditional reactive and preventive approaches. Reactive maintenance waits for failure. Preventive maintenance follows a schedule. Condition-based maintenance acts when a measured condition crosses a defined threshold. Predictive maintenance goes further: it uses historical data, real-time condition data, and models for failure forecasting – estimating future failure risk or remaining useful life.
IBM defines predictive maintenance as an approach that builds on condition-based monitoring by continually assessing equipment health in real time to optimize performance and lifespan. AWS describes it as a strategy for estimating and planning operational equipment maintenance schedules. SAP describes the process as collecting data from assets, transmitting it in real time, applying AI or machine learning, and taking action based on the resulting insight.
Predictive maintenance is used in manufacturing, oil and gas, automotive, rail, energy, aerospace, mining, utilities, logistics, and other asset-intensive industries. Its purpose is not to replace maintenance teams. Its purpose is to give them better timing, better evidence, and a clearer connection between asset health and operational risk.
What is predictive maintenance?
Predictive maintenance, often abbreviated as PdM, is a proactive maintenance strategy that uses data to estimate equipment condition and predict when maintenance will be needed. It is condition-based, because it relies on the state of the asset, and data-driven, because the decision is based on sensor data, maintenance history, operating conditions, and analytical models.
A predictive maintenance system typically monitors signals such as:
- vibration,
- temperature,
- pressure,
- current,
- oil condition,
- acoustic emission,
- speed,
- load,
- operating hours,
- alarms,
- maintenance history.
These signals are analyzed to detect degradation patterns, estimate failure probability, or calculate remaining useful life. The output should not be just a chart or alert. A mature predictive maintenance process should lead to a maintenance decision: inspect, lubricate, adjust, plan a work order, order parts, schedule downtime, or continue monitoring.
This is an important distinction. Predictive maintenance is not the same as simply installing sensors. Sensors provide data. Predictive maintenance turns that data into a decision before failure occurs.
Predictive maintenance meaning in manufacturing
In manufacturing, predictive maintenance means using machine and process data to reduce unplanned downtime, improve asset availability, and plan maintenance around production needs. It is most valuable for equipment where failure is costly, safety-critical, quality-critical, or difficult to repair under time pressure.
Common manufacturing assets include:
- motors,
- pumps,
- compressors,
- gearboxes,
- conveyors,
- fans,
- turbines,
- spindles,
- presses,
- ovens,
- packaging machines,
- welding robots,
- CNC machines,
- industrial drives.
Predictive maintenance in manufacturing often depends on data from PLCs, SCADA systems, MES, historians, IoT sensors, CMMS, EAM, and quality systems. Machine condition data shows how the asset is behaving. Production context shows what product, order, shift, load, or process state was active when the signal changed.
That context matters. A motor temperature increase may be normal under high load but abnormal under stable operating conditions. A vibration increase may be expected after a process change but significant if it appears during normal operation. Predictive maintenance becomes more useful when it combines condition data with operational context.
For broader factory visibility, PdM can be linked to production monitoring, but production monitoring itself is a separate topic. PdM can also influence OEE Availability by reducing unplanned stops, but the OEE formula should be covered in a dedicated OEE guide.
The four maintenance strategies compared
Predictive maintenance is one of several maintenance strategies. It is easiest to understand when compared with reactive, preventive, and condition-based maintenance.
| Strategy | Approach | Timing | Data basis | Best for |
| Reactive maintenance | Run to failure | After breakdown | None or minimal | Non-critical, cheap, easily replaceable assets |
| Preventive maintenance | Calendar- or usage-based service | Scheduled intervals | Manufacturer recommendations, experience, operating hours | Equipment without sensors or predictable wear patterns |
| Condition-based maintenance | Threshold-based intervention | When condition limits are exceeded | Real-time sensor data and defined thresholds | Monitored assets with clear condition limits |
| Predictive maintenance | Failure forecasting | Before predicted failure | Sensor data, historical failures, ML models, asset context | Critical, expensive, safety- or production-critical assets |
Reactive maintenance can be acceptable for low-cost assets where failure has little operational impact. Preventive maintenance is useful when failure patterns are time- or usage-dependent and when sensor coverage is limited. Condition-based maintenance is effective when there are clear measurable thresholds. Predictive maintenance is most useful when the organization wants to forecast degradation before the asset crosses a critical limit.
Predictive maintenance is often described as an advanced form of condition-based maintenance. Condition-based maintenance asks: has the condition crossed a threshold? Predictive maintenance asks: what is likely to happen next, and when?
Some organizations extend predictive maintenance into prescriptive maintenance, where the system not only predicts failure but recommends or automatically initiates specific corrective actions. Prescriptive maintenance combines prediction models with optimization algorithms, decision rules, and sometimes digital twin simulation to suggest the most effective response. This article focuses on predictive maintenance; prescriptive maintenance is covered in a dedicated guide.
Predictive maintenance vs preventive maintenance
The main difference between predictive and preventive maintenance is the timing logic. Preventive maintenance is schedule-driven. Predictive maintenance is condition- and forecast-driven.
Preventive maintenance might replace a bearing every six months because the calendar says so. Predictive maintenance would analyze vibration, temperature, load, and historical failure patterns to determine whether that bearing is still healthy or whether it is entering a failure window.
This difference matters because preventive maintenance can create two types of waste:
- replacing parts too early,
- missing failures that occur before the scheduled interval.
Predictive maintenance aims to reduce both risks. It schedules work when evidence suggests it is needed, not simply because a fixed date has arrived.
This does not mean preventive maintenance is obsolete. Many manufacturers use both. Safety checks, statutory inspections, lubrication routines, and compliance tasks may still follow planned intervals. Predictive maintenance is usually applied first to critical assets where failure risk and downtime cost justify the data and system investment.
| Criterion | Preventive Maintenance | Predictive Maintenance |
| Timing logic | Calendar/usage schedule | Condition + forecast |
| Data requirement | Minimal (OEM recommendations) | Sensors, historical failures, ML |
| Cost of over-maintenance | High (unnecessary part replacements) | Low (evidence-based scheduling) |
| Cost of under-maintenance | Medium (failures between intervals) | Low (continuous monitoring) |
| Best for | Assets with time-dependent wear | Critical assets with detectable degradation |
| Typical ROI driver | Reduced emergency repairs | Avoided unplanned downtime |
| Implementation complexity | Low | Medium-High |
Predictive maintenance vs reactive maintenance
Reactive maintenance means repairing equipment after it fails. It is simple, but it can be expensive when failures interrupt production, damage connected equipment, create safety risks, or require emergency spare parts.
Predictive maintenance is a proactive alternative to reactive maintenance. It tries to identify potential failure before the asset reaches functional failure. The goal is not to eliminate every failure. The goal is to make more failures visible early enough to plan action.
For example, a pump may show increasing vibration several weeks before failure. A reactive approach waits until the pump stops. A predictive approach flags the trend, estimates risk, and triggers inspection or work order planning while production can still choose the least disruptive maintenance window.
This is where predictive maintenance supports asset management strategy. It gives maintenance and operations teams more time to plan, prioritize, and coordinate.
How predictive maintenance works?
Predictive maintenance works through a sequence of data collection, analysis, alerting, and action. A common flow is:
sensor → data stream → model → alert → work order → feedback
In practice, the process looks like this:
- Sensors collect data from equipment.
- Edge devices or gateways transmit data to a platform.
- Data is stored, cleaned, and contextualized.
- Analytics or machine learning models detect degradation patterns.
- The system predicts failure probability or remaining useful life.
- A predictive maintenance alert is generated.
- A CMMS or EAM creates or updates a work order.
- Maintenance action is completed.
- The outcome is fed back into the model and asset history.
SAP describes a four-stage architecture for predictive maintenance and industrial IoT: collecting data from sensors, transmitting it in real time, applying AI and machine learning, and taking action through automated or human response.
A predictive maintenance system should therefore include both analytical and operational layers. A model that predicts a problem is useful only if the organization can act on the prediction. That usually requires integration with maintenance planning, spare parts inventory, work orders, and production scheduling.
Data sources used in predictive maintenance
Predictive maintenance depends on equipment data, operating context, and historical outcomes. The most common data sources are:
| Data source | Typical signals | Predictive maintenance use |
| Vibration sensors | acceleration, velocity, frequency spectrum | bearing wear, imbalance, misalignment, looseness |
| Temperature sensors | surface temperature, bearing temperature, motor temperature | overheating, lubrication issues, electrical problems |
| Pressure sensors | pressure changes, pressure drops, fluctuations | leaks, blockages, pump or compressor issues |
| Current and voltage | current signature, load, power quality | motor faults, drive issues, insulation degradation |
| Oil and fluid data | viscosity, particle count, wear metals, water contamination | lubrication degradation, internal wear |
| Acoustic and ultrasonic data | high-frequency sound, acoustic emission | leaks, partial discharge, early bearing faults |
| SCADA and PLC data | states, alarms, process values, cycles | operating context and event history |
| CMMS and EAM data | work orders, failure codes, repairs, parts | historical maintenance and failure outcomes |
| MES data | orders, products, operations, batches | production context and asset usage |
| Historian data | time-series trends | long-term operating patterns |
Historical failure data is particularly valuable for supervised machine learning. If the organization knows when failures occurred and what signals preceded them, models can learn patterns associated with future failures. In many companies, however, failure history is incomplete, inconsistent, or recorded only in text work orders. That is one reason predictive maintenance projects often begin with data preparation before model building.
Predictive maintenance techniques
Predictive maintenance uses several monitoring techniques. The right technique depends on the asset type, failure mode, operating environment, and P-F interval.
Vibration analysis
Vibration analysis is one of the most common predictive maintenance techniques for rotating equipment. It uses accelerometer sensors to detect patterns associated with imbalance, misalignment, mechanical looseness, bearing wear, gear defects, resonance, and other mechanical problems.
Vibration signals are often analyzed in the frequency domain using FFT, or Fast Fourier Transform. FFT converts a time-domain vibration signal into frequency components, making it easier to identify characteristic fault frequencies.
Vibration analysis is especially relevant for:
- motors,
- pumps,
- compressors,
- fans,
- gearboxes,
- turbines,
- spindles,
- rotating shafts.
ISO 20816 establishes general conditions and procedures for measuring and evaluating machine vibration, and ISO 10816 is an older related series used for vibration evaluation on non-rotating machine parts.
Vibration analysis often detects degradation earlier than thermal methods because mechanical faults can appear in the vibration signature before they generate significant heat. This is why vibration is frequently shown earlier on the P-F curve.
Thermal and infrared analysis
Thermal analysis uses infrared thermography or temperature sensors to detect abnormal heat patterns. It is a non-contact technique when performed with infrared cameras, and it is widely used for electrical systems, mechanical components, insulation problems, blockages, friction, and cooling issues.
Typical applications include:
- electrical panels,
- motors,
- bearings,
- steam systems,
- furnaces,
- refractory lining,
- heat exchangers,
- blocked pipes,
- overheating connections.
Thermal analysis is useful because heat is a visible symptom of stress, resistance, friction, overload, or blocked flow. It may not always detect the earliest sign of failure, but it is practical, fast, and useful across many asset types.
Oil and fluid analysis
Oil analysis monitors the condition of lubricants and the equipment they protect. It can measure viscosity, particle count, water contamination, oxidation, additive depletion, and wear metals through methods such as spectroscopy.
Oil analysis is especially relevant for:
- gearboxes,
- engines,
- hydraulic systems,
- turbines,
- compressors,
- lubricated bearings,
- heavy mobile equipment.
For example, increasing iron, copper, or chromium particles may indicate wear of internal components. Water contamination may indicate sealing issues. A change in viscosity may point to lubricant degradation or contamination.
Oil analysis is valuable because the lubricant often carries evidence of internal wear before the asset fails functionally.
Ultrasonic and acoustic analysis
Ultrasonic and acoustic analysis detects sound patterns, especially high-frequency signals that are not always audible to humans. It can be airborne or structure-borne.
Typical applications include:
- compressed air leaks,
- vacuum leaks,
- steam trap issues,
- bearing faults,
- lubrication issues,
- partial discharge in electrical systems.
Ultrasonic inspection is useful in noisy industrial environments because high-frequency signals can be isolated from lower-frequency background noise. It is often used as a practical technique for leak detection and early-stage bearing fault detection.
Electrical monitoring
Electrical monitoring analyzes voltage, current, power quality, insulation resistance, and motor current signature patterns. Motor Current Signature Analysis, or MCSA, can help identify motor and drive-related faults by detecting abnormal patterns in current.
Typical applications include:
- motors,
- drives,
- pumps,
- compressors,
- conveyors,
- electrical cabinets,
- insulation systems.
Electrical monitoring can identify issues such as rotor bar defects, stator problems, imbalance, overload, power quality issues, or insulation degradation. It is particularly valuable where mechanical access is difficult but electrical measurements are available.
The P-F curve
The P-F curve is one of the most important concepts in predictive maintenance. It describes the interval between the earliest detectable sign of a problem and the point where the asset can no longer perform its required function.
- P = potential failure: the earliest detectable sign that degradation has started.
- F = functional failure: the point where the asset no longer performs its required function.
- P-F interval: the time window available to detect, plan, and act before failure.
The value of predictive maintenance depends on detecting problems inside the P-F interval early enough to take action. A longer P-F interval gives maintenance teams more time to plan work, order spare parts, coordinate with production, and avoid emergency repair.
Different techniques detect failures at different points on the P-F curve. Vibration analysis may detect mechanical degradation early. Oil analysis may reveal internal wear before vibration becomes severe. Thermal analysis may detect later-stage friction or electrical heating. Ultrasonic analysis may detect leaks or partial discharge early in specific applications.
Condition monitoring maps detection points on the P-F curve, but the full condition monitoring methodology should be covered in a dedicated condition monitoring guide.
Remaining Useful Life (RUL)
Remaining Useful Life, or RUL, is the predicted time until an asset reaches functional failure. It is one of the key outputs of predictive maintenance models.
RUL can be expressed in:
- hours,
- cycles,
- days,
- production batches,
- distance,
- operating events,
- probability bands.
For example, a model may predict that a bearing has 120 operating hours before failure risk becomes unacceptable. Another model may classify an asset into a time-to-failure band such as “0–7 days,” “8–30 days,” or “more than 30 days.”
RUL models can be:
- regression-based, predicting a continuous time value,
- classification-based, predicting a risk category or time window,
- physics-informed, using degradation equations and engineering knowledge,
- data-driven, using historical sensor and failure data,
- hybrid, combining physical knowledge with machine learning.
RUL should not be treated as a precise guarantee. It is a planning signal. Its usefulness depends on data quality, failure mode consistency, operating conditions, model validation, and maintenance feedback.
When integrated with CMMS or EAM, RUL can trigger work order scheduling, spare parts planning, and production coordination.
Machine learning for predictive maintenance
Machine learning is the analytical engine in many predictive maintenance systems. It analyzes sensor streams, historical failures, operating context, and maintenance outcomes to detect patterns that are difficult to capture with fixed rules.
Common machine learning approaches include:
| Model type | Typical output | PdM use |
| Classification | fault / no fault, failure type, risk category | identify whether an asset is likely to fail |
| Regression | continuous value | estimate remaining useful life |
| Anomaly detection | deviation from normal behavior | flag unusual equipment behavior |
| Clustering | groups of similar behavior | identify operating modes or hidden patterns |
| Time series forecasting | predicted future values | forecast degradation trends |
| Deep learning | learned features from raw data | analyze complex signals, vibration, sound, images |
Supervised learning uses labeled historical examples, such as past failures and preceding sensor data. Unsupervised learning can be used when failure labels are limited, using anomaly detection or clustering to identify abnormal operating patterns. Deep learning methods such as LSTM models may be used for sequential time-series data, while CNNs can be applied to signal representations or images.
Feature engineering is often as important as model selection. Useful features may include vibration RMS, kurtosis, peak values, frequency bands, temperature gradients, pressure fluctuation, load-normalized current, or trend rates.
Anomaly detection and time series analysis are important parts of PdM, but they deserve dedicated treatment in separate articles on anomaly detection and time series analysis.
IoT sensors and edge computing in predictive maintenance
Predictive maintenance IoT refers to the use of connected industrial sensors, edge devices, and data platforms to monitor asset health continuously or near-real time.
Typical IoT sensor types include:
- wireless vibration sensors,
- temperature sensors,
- pressure sensors,
- acoustic sensors,
- current sensors,
- oil condition sensors,
- humidity sensors,
- speed sensors.
Sampling frequency depends on the signal. Some values may be collected every few seconds or minutes. Vibration and acoustic data may require millisecond-level sampling or high-frequency acquisition, especially when frequency analysis is needed.
Edge computing is used when data needs to be processed close to the machine. An edge gateway can filter signals, calculate features, compress data, detect local anomalies, buffer data during network outages, and transmit selected streams to cloud or on-premise platforms.
Common industrial communication patterns include MQTT, OPC UA, REST APIs, historian connectors, and streaming pipelines. AWS describes IoT devices and smart sensors as part of predictive maintenance strategies for monitoring machinery performance.
IoT is the data collection layer for predictive maintenance. It does not replace reliability engineering, failure mode analysis, or maintenance planning. It makes the data available so those decisions can be better timed.
CMMS and EAM integration
Predictive maintenance must connect to maintenance execution. That usually means integration with a CMMS or EAM system.
A CMMS, or Computerized Maintenance Management System, manages maintenance work orders, tasks, schedules, spare parts, and maintenance history. EAM, or Enterprise Asset Management, typically covers a broader asset lifecycle, including asset hierarchy, cost, compliance, risk, and long-term performance.
In predictive maintenance, CMMS/EAM integration enables:
- automatic work order generation from PdM alerts,
- asset hierarchy mapping,
- maintenance history analysis,
- spare parts planning,
- technician assignment,
- feedback on completed work,
- tracking of false positives and missed failures.
Without CMMS or EAM integration, predictive maintenance alerts can remain isolated from daily maintenance execution. The system may identify a problem, but the organization may fail to turn the alert into scheduled work.
IBM Maximo is one example of an enterprise asset management platform positioned around asset management, maintenance optimization, AI insights, and reliability workflows, with deployment options including client-managed software and SaaS.
Predictive maintenance in manufacturing: MES, SCADA, and asset context
Predictive maintenance in manufacturing works best when asset condition data is connected with production context. A vibration signal alone may show that a bearing is deteriorating, but production data can explain whether the asset was under unusual load, producing a specific product, running after a changeover, or operating during an abnormal process state.
Useful manufacturing context includes:
- asset hierarchy,
- line and machine,
- production order,
- product,
- batch,
- recipe,
- speed,
- load,
- operator shift,
- maintenance history,
- quality results,
- alarms,
- OEE Availability events.
MES provides production context. SCADA provides equipment and process states. Historians provide time-series history. CMMS provides work history. A predictive maintenance platform connects these data sources so the model can understand not only the signal, but the operating situation.
This is where an industrial data platform can support PdM: it can connect OT and IT data, map signals to assets, provide event context, and feed results into maintenance workflows. Smart RDM, for example, is positioned as an Industrial Data & AI Platform that can connect industrial data, analytics, reporting, knowledge management, and operational decision support in one environment.
Digital twins can also be used in PdM to represent assets, simulate behavior, or contextualize degradation patterns, but digital twin architecture is a separate topic covered in a dedicated digital twin guide.
Benefits and ROI of predictive maintenance
Predictive maintenance benefits should be evaluated in operational and financial terms. The most commonly cited benefits include reduced unplanned downtime, better asset availability, improved maintenance planning, lower emergency repair costs, longer equipment life, and better spare parts management.
SAP’s overview cites reported benefits from predictive maintenance programs, including up to 15% downtime reduction, up to 20% labor productivity increase, and up to 30% inventory reduction.
The same SAP source lists industry examples, including oil and gas maintenance cost reductions of up to 38%, automotive welding robots generating millions of data points for predictive accuracy, rail void detection for safety, and a steel industry example reporting a 60% equipment lifetime improvement.
Typical benefit areas include:
| Benefit area | How PdM contributes |
| Downtime | detects degradation before breakdown |
| Maintenance labor | shifts work from emergency repair to planned work |
| Spare parts | improves inventory planning and reduces emergency purchases |
| Asset life | avoids running equipment into severe failure states |
| Safety | reduces failure risk in critical assets |
| Production planning | coordinates maintenance with production windows |
| Quality | detects equipment degradation that may affect product quality |
| Energy | identifies inefficient operation linked to asset degradation |
Energy can be affected by asset condition, but energy optimization should be handled as a dedicated energy optimization topic.
ROI should be calculated asset by asset or asset class by asset class. The business case is strongest when failure cost is high, failure modes are detectable, and the organization can act within the P-F interval.
A practical ROI formula for predictive maintenance is:
Annual avoided failure cost + annual maintenance labor savings + annual spare parts savings − annual PdM operating cost = annual net benefit.
Annual net benefit ÷ total PdM investment = ROI.
For critical rotating assets, a common benchmark range for PdM ROI is 5:1 to 10:1 over three to five years.
Challenges of predictive maintenance
Predictive maintenance is not just a software purchase. It is an operational change that requires data, reliability knowledge, sensors, workflows, and adoption by maintenance teams.
Common challenges include:
High initial cost
Sensors, gateways, software, integration, and engineering effort can be expensive. PdM should start with critical assets where failure cost justifies the investment.
Data quality
Poor data quality can produce unreliable predictions. Missing sensor data, inconsistent failure codes, wrong timestamps, and incomplete maintenance history all reduce model quality.
Sensor calibration and placement
Sensor placement affects signal quality. A poorly installed accelerometer can produce misleading vibration readings. Temperature sensors, current sensors, and acoustic sensors also need correct placement and calibration.
Historical data dependency
Supervised machine learning models require examples of failures. Many plants do not have enough labeled failure data, or the failure records are stored in unstructured work order notes.
Workforce training
Maintenance teams must understand what predictive alerts mean, how to validate them, and how to act on them. Without training, alerts may be ignored or overtrusted.
False positives and false negatives
A false positive creates unnecessary inspection or maintenance. A false negative misses a real failure. Both must be tracked and used to improve model performance.
Integration gaps
If alerts are not connected to CMMS, EAM, spare parts, and production scheduling, predictions may not translate into action.
Change management
Predictive maintenance changes the way maintenance is planned. Teams used to fixed schedules or emergency response may need time to trust data-driven work planning.
How to implement predictive maintenance?
A practical predictive maintenance implementation should be staged. Starting too broadly can lead to sensor overload, poor adoption, and unclear ROI.
Step 1: Identify critical assets
Start with assets where failure has a measurable impact on production, safety, quality, cost, or delivery. Use asset criticality, maintenance history, downtime cost, and reliability risk to prioritize.
FMEA, or Failure Mode and Effects Analysis, can help identify which failure modes are important and whether they are detectable early enough for predictive maintenance.
Step 2: Define failure modes and monitoring techniques
Predictive maintenance should be failure-mode driven. For a rotating motor, vibration and current monitoring may be appropriate. For a hydraulic system, oil analysis and pressure monitoring may matter more. For an electrical panel, thermography and electrical monitoring may be more relevant.
Step 3: Install sensors and collect baseline data
Install the required sensors and collect baseline data under normal operating conditions. Baseline data helps define what “normal” looks like for each asset, product, load, and operating state.
Step 4: Connect data through edge or platform infrastructure
Use edge gateways, historians, cloud platforms, or on-premise platforms to collect and manage the data. Protocols such as MQTT and OPC UA are common in industrial environments.
Step 5: Build rules or models
Start with simple thresholds or expert rules if historical failure data is limited. Add machine learning models when enough data exists to support classification, regression, anomaly detection, or RUL prediction.
Step 6: Integrate with CMMS or EAM
A predictive alert should trigger a maintenance workflow. Integration with CMMS or EAM enables work order generation, task planning, spare parts reservation, and technician assignment.
Step 7: Monitor, validate, and improve
Track prediction accuracy, false positives, missed failures, maintenance outcomes, and business impact. Feed results back into the model and asset history.
A useful implementation rule is: start with a narrow asset class, prove value, then scale. Predictive maintenance succeeds when the organization learns how to close the loop from signal to action.
Industry examples and use cases
Manufacturing
In manufacturing, predictive maintenance is used to reduce unplanned downtime on production-critical equipment. Examples include monitoring motors, gearboxes, conveyors, compressors, packaging machines, presses, spindles, and robots. PdM supports equipment uptime and can improve OEE Availability without expanding into the full OEE calculation.
Oil and gas
Oil and gas assets operate in harsh environments where failure can be expensive and safety-critical. SAP’s overview cites an oil and gas example where monitoring oil temperature and gearbox speed in drilling equipment reduced maintenance costs by up to 38%.
Automotive
Automotive manufacturing uses predictive maintenance for welding robots, assembly systems, conveyors, paint shops, machining centers, and stamping equipment. SAP describes an automotive case where connected spot-welding guns generate millions of data points used to improve predictive accuracy.
Rail
Rail applications include track and rolling stock monitoring. Predictive maintenance can support void detection, wheel and bearing monitoring, braking systems, and infrastructure safety. SAP describes rail void detection as an example of predictive maintenance supporting operational safety.
Steel
Steel manufacturing uses vibration, rotational speed, and electrical current data for assets such as cold-rolling equipment. SAP cites a steel example where anomaly detection contributed to a 60% improvement in equipment lifetime.
Energy and utilities
Energy and utility applications include turbine monitoring, generator condition monitoring, transformer monitoring, wind turbine vibration analysis, and grid asset reliability. The sector often uses PdM to manage high-value, safety-critical assets.
Aerospace
Aerospace uses predictive maintenance for engine health monitoring, component reliability, and aircraft maintenance planning. The focus is often safety, reliability, and lifecycle cost rather than only downtime reduction.
Mining
Mining equipment operates under heavy loads, dust, vibration, and harsh environmental conditions. Predictive maintenance can support haul trucks, conveyors, crushers, mills, pumps, and mobile assets.
Predictive maintenance software and vendor landscape 2026
Predictive maintenance software ranges from enterprise asset platforms and cloud AI services to industrial IoT platforms, fleet systems, MES-connected applications, and domain-specific monitoring tools.
The following landscape is neutral and informational. It is not a ranking.
| Vendor / source | Positioning | Typical role |
| IBM | Enterprise predictive maintenance and asset management, including Maximo | EAM, AI insights, asset reliability, maintenance workflows |
| SAP | Asset performance management and predictive maintenance overview | Enterprise asset strategy, APM, business integration |
| Wikipedia | Encyclopedia-level definition | General reference |
| Splunk | IT/OT observability and data analysis | Observability and operational data analytics |
| QAD | ERP/MES-related manufacturing operations context | Manufacturing systems and enterprise operations |
| AWS | Cloud predictive maintenance using IoT and machine learning services | Cloud, IoT, sensor data, model development |
| Geotab | Vehicle and fleet predictive maintenance | Fleet and transport asset monitoring |
| Brewer Science | Manufacturing-oriented predictive maintenance content | Industrial use case education |
| PTC | ThingWorx and IIoT-based predictive maintenance | Industrial IoT and connected assets |
| Smart RDM | Industrial Data & AI Platform | Industrial data integration, analytics, AI, and operational decision support |
PTC positions ThingWorx as an industrial IoT platform that applies predictive analytics to help manufacturers move from reactive to proactive maintenance. AWS positions predictive maintenance around IoT devices, smart sensors, and machine learning for monitoring equipment performance.
When selecting predictive maintenance software, manufacturers should evaluate:
- asset coverage,
- sensor support,
- edge and cloud deployment options,
- CMMS/EAM integration,
- support for OPC UA and MQTT,
- model transparency,
- alert management,
- RUL prediction,
- data governance,
- cybersecurity,
- multi-site scalability,
- connection to production context.
The best tool depends on whether the organization needs a narrow monitoring tool, a CMMS-integrated workflow, an enterprise asset platform, or a broader industrial data platform.
Predictive maintenance tools: what should be included?
A predictive maintenance system usually includes several layers rather than one standalone tool.
| Layer | Examples |
| Data acquisition | sensors, PLCs, gateways, historians |
| Connectivity | OPC UA, MQTT, APIs, streaming |
| Storage | time-series database, historian, data lakehouse |
| Analytics | rules, ML models, anomaly detection, RUL models |
| Visualization | dashboards, alerts, trend views |
| Execution | CMMS, EAM, work orders, spare parts |
| Feedback | repair confirmation, failure labels, model retraining |
A useful predictive maintenance tool should not only detect abnormal data. It should help maintenance teams understand the asset, the failure mode, the risk, the recommended action, and the work process required to resolve it.
Predictive maintenance and generative AI
Generative AI can support predictive maintenance by helping users interpret maintenance history, equipment manuals, alarm logs, work orders, and diagnostic recommendations. It can also support natural-language access to maintenance knowledge.
For example, a technician might ask:
“Why did this compressor trigger a bearing alert?”
A useful answer would combine sensor trends, failure history, operating context, and relevant maintenance documentation. However, generative AI should not replace engineering validation. It should support human decision-making, especially in safety- or production-critical environments.
This is where retrieval-augmented generation, semantic search, and controlled knowledge sources can be useful. The full topic belongs in a broader article on AI in manufacturing or industrial knowledge management.
References and further reading
Predictive maintenance definitions and implementation concepts are covered by IBM, AWS, and SAP. IBM describes PdM as real-time assessment of equipment health; AWS frames it as estimating and planning operational equipment maintenance; SAP explains the IoT and AI workflow from sensors to action.
For vibration monitoring, ISO 20816 provides general conditions and procedures for machine vibration measurement and evaluation, while ISO 10816 is an older related vibration evaluation series.
For condition monitoring software and information handling, ISO 13374 provides guidelines for data processing, communication, and presentation of machine condition monitoring and diagnostic information.
In semiconductor and high-tech manufacturing, SEMI E10 defines basic equipment conditions, reliability, availability, maintainability, and utilization measurement.
FAQ
What is predictive maintenance?
Predictive maintenance is a data-driven maintenance strategy that uses sensor data, equipment condition, historical failures, and analytical models to predict when maintenance should be performed before functional failure occurs.
What is the predictive maintenance definition?
Predictive maintenance is a proactive, condition-based maintenance strategy that forecasts failure risk or remaining useful life using real-time equipment data and historical maintenance information.
What is predictive maintenance meaning in manufacturing?
In manufacturing, predictive maintenance means using machine data, production context, and maintenance history to reduce unplanned downtime and schedule maintenance before critical equipment fails.
What are the four types of maintenance?
The four commonly compared maintenance strategies are reactive maintenance, preventive maintenance, condition-based maintenance, and predictive maintenance.
What are the three types of predictive maintenance?
The phrase is used differently, but common predictive maintenance technique groups include vibration analysis, thermal or infrared analysis, and oil or fluid analysis. Ultrasonic analysis and electrical monitoring are also widely used.
What is the difference between predictive and preventive maintenance?
Preventive maintenance is calendar- or usage-based. Predictive maintenance is condition- and forecast-based. Preventive maintenance acts on a schedule, while predictive maintenance acts when data indicates future failure risk.
What is condition-based maintenance?
Condition-based maintenance triggers maintenance when measured equipment conditions cross thresholds. Predictive maintenance builds on this by forecasting future failure probability or remaining useful life.
How does predictive maintenance work?
Predictive maintenance works by collecting sensor data, transmitting it through edge or platform infrastructure, analyzing it with rules or machine learning models, generating alerts, and triggering maintenance action through CMMS or EAM workflows.
What is the P-F curve?
The P-F curve describes the interval between potential failure and functional failure. Predictive maintenance tries to detect problems early in that interval so teams have time to plan corrective action.
What is RUL?
RUL stands for Remaining Useful Life. It is the predicted time, cycles, or operating period until an asset is expected to reach functional failure.
What is vibration analysis in predictive maintenance?
Vibration analysis uses accelerometers and signal processing, often including FFT, to detect mechanical issues such as imbalance, misalignment, looseness, bearing wear, and gearbox faults.
What is thermal analysis in predictive maintenance?
Thermal analysis uses infrared thermography or temperature sensors to detect heat patterns, hotspots, electrical faults, blockages, friction, or cooling problems.
What is oil analysis in predictive maintenance?
Oil analysis evaluates lubricant condition and equipment wear using indicators such as viscosity, particle count, water contamination, spectroscopy, and wear metals.
What is ultrasonic analysis in predictive maintenance?
Ultrasonic analysis detects high-frequency sound patterns and is used for leak detection, bearing faults, lubrication issues, and partial discharge in electrical systems.
What is electrical monitoring in predictive maintenance?
Electrical monitoring analyzes voltage, current, power quality, insulation resistance, and motor current signature patterns to detect motor, drive, and electrical system issues.
What is predictive maintenance IoT?
Predictive maintenance IoT uses connected sensors, edge gateways, and data platforms to collect equipment condition data and transmit it for analysis, alerting, and maintenance planning.
How is machine learning used in predictive maintenance?
Machine learning is used for fault classification, remaining useful life prediction, anomaly detection, clustering, and time series forecasting based on sensor and historical failure data.
What is CMMS in predictive maintenance?
A CMMS manages work orders, maintenance schedules, spare parts, and asset history. In predictive maintenance, CMMS integration turns predictive alerts into maintenance actions.
What are predictive maintenance benefits?
Predictive maintenance can reduce downtime, improve labor productivity, optimize spare parts inventory, extend asset life, improve safety, and support maintenance planning. SAP cites reported benefits including up to 15% downtime reduction, up to 20% labor productivity increase, and up to 30% inventory reduction.
What are predictive maintenance challenges?
Common challenges include high initial cost, poor data quality, limited failure history, sensor calibration, integration gaps, false alerts, workforce training, and difficulty turning predictions into work orders.
How do you implement predictive maintenance?
Implementation usually follows these steps: identify critical assets, define failure modes, select monitoring techniques, install sensors, collect baseline data, build models, integrate with CMMS or EAM, monitor performance, and improve over time.
What is predictive maintenance in AI?
Predictive maintenance in AI uses machine learning, statistical models, and sometimes generative AI to analyze equipment data, detect degradation, estimate remaining useful life, and support maintenance decisions.
What is TPM and PPM?
TPM stands for Total Productive Maintenance, a maintenance and production improvement approach focused on equipment effectiveness. PPM is often used to mean Planned Preventive Maintenance, but terminology varies by organization.
Conclusion
Predictive maintenance helps maintenance teams move from fixed schedules and emergency repairs toward evidence-based planning. It uses sensor data, operating context, machine learning, and maintenance history to detect degradation before functional failure.
Its value depends on more than models. A predictive maintenance system needs reliable sensors, clean data, relevant failure modes, a usable P-F interval, CMMS or EAM integration, trained users, and feedback from real maintenance outcomes.
For manufacturers and other asset-intensive organizations, predictive maintenance works best when it is focused on critical assets, connected to real operating data, and embedded in maintenance workflows. The result is not just earlier failure detection. It is better coordination between production, maintenance, reliability, and asset management.
Light mode